


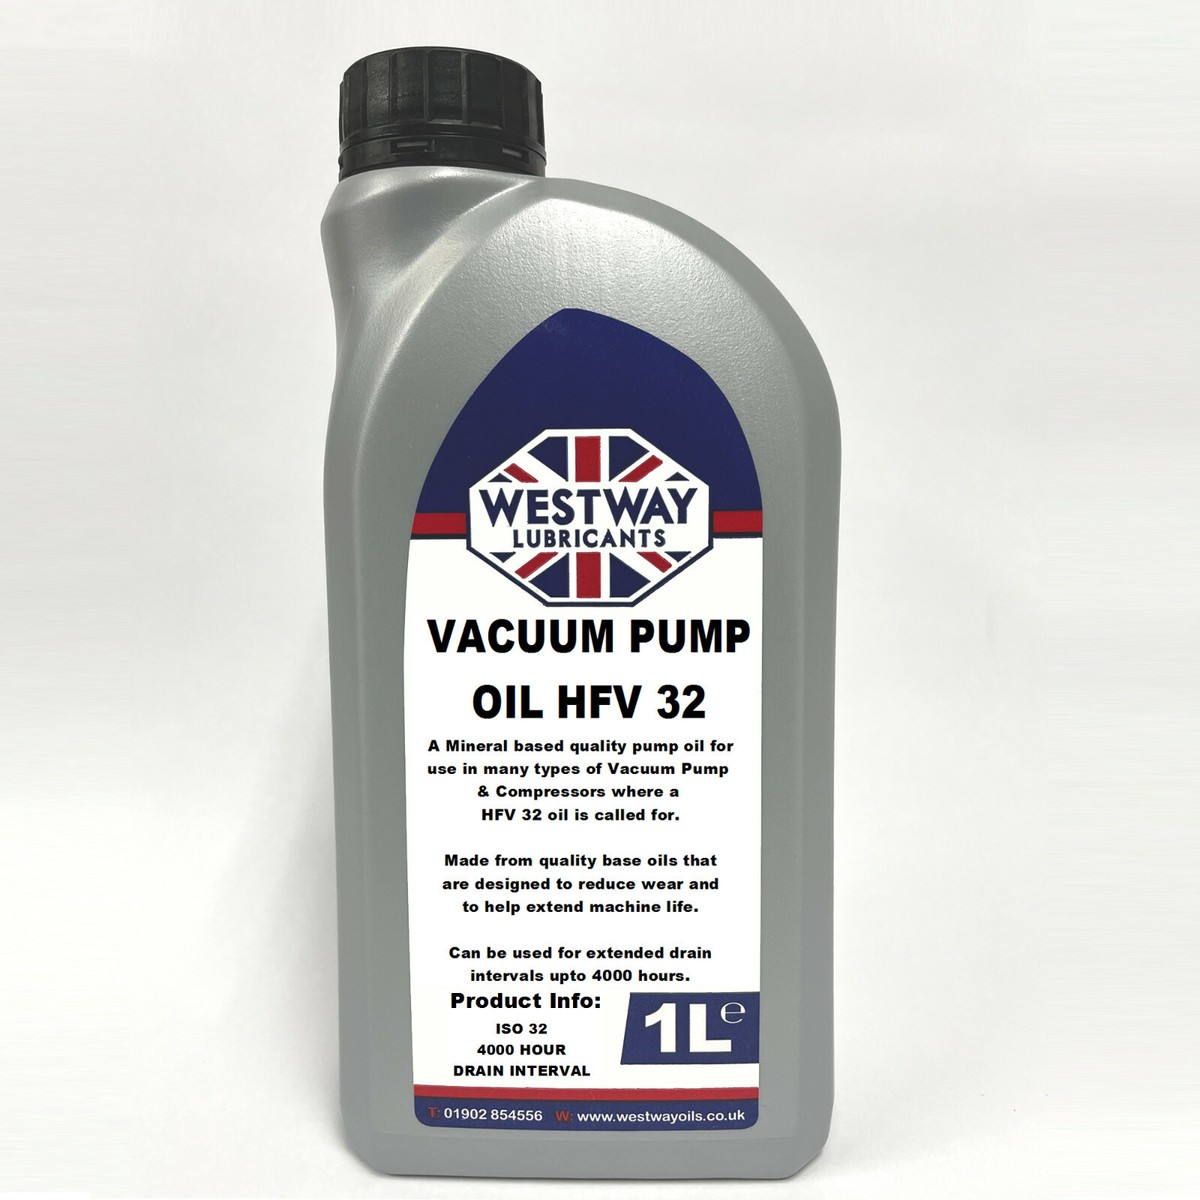

Enhanced Capacity: Industrial-grade precision volume delivering high-efficiency evacuation economy and consistent deep-vacuum yields for precision maintenance operations.
Optimal Energy Efficiency: Advanced low-vapor-pressure technology maximizes sealing coefficients, ensuring reduced evacuation time draw for heavy-duty vacuum pumps.
Single-Component Fluid: Highly stable refined mineral profile across mass maintenance cycles, ensuring reliable deployment for continuous enterprise usage.
Eco-Friendly Alternative: Long-term sustainable design with zero contamination-transfer risks, built to withstand demanding industrial maintenance loads.
Authenticity Guaranteed: Regulated factory assembly ensures no mechanical debris inside sensitive, high-capacity refrigeration circuits.
Applications:
Large-scale commercial food processing cold stores.
Multi-compressor industrial refrigeration distribution hubs.
High-demand retail display and backup storage infrastructure.
Technical Specifications
| Attribute | Detail |
| Brand | Industrial Std |
| Trade Name | Vacuum Pump Oil |
| Model | VPO-1L |
| Capacity | 1 Liter |
| Application | Pump Evacuation Maintenance |
| Country of Origin | Global Standard |
Logistics & Shipping
Net Weight: 0.9 kg
Gross Weight: Approx. 1.1 kg
Packaging Dimension: 12.0 cm x 12.0 cm x 20.0 cm
Shipping Method: Industrial Freight. Warning: Change oil frequently after deep evacuations for maximum pump efficiency and retention.
Market Insight: A trusted, budget-friendly bulk solution widely utilized by large-scale commercial cold room operators across Nigeria to manage massive inventory volumes while effectively controlling operational overhead.


