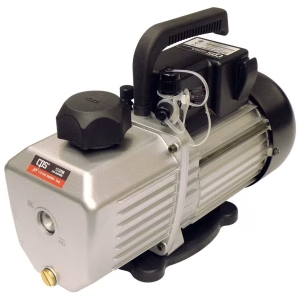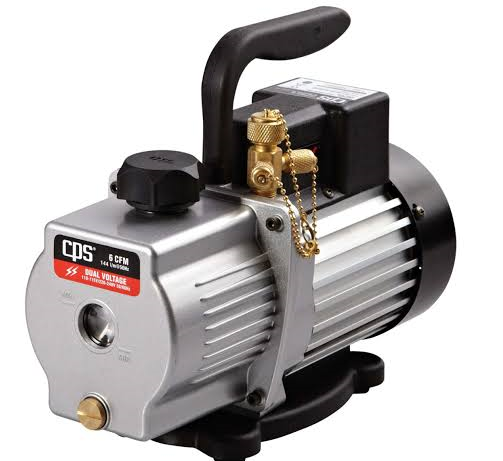

(Enhanced Capacity: Industrial-grade protected heavy-duty volume delivering high-efficiency high-volume evacuation economy and robust protection yields for large-scale operations.
Optimal Energy Efficiency: Advanced roll-cage motor protection technology maximizes durability coefficients, ensuring reduced impact damage for heavy-duty pumps.
Single-Component Fluid: Highly stable armored-chassis profile across mass maintenance cycles, ensuring reliable deployment for continuous enterprise usage.
Eco-Friendly Alternative: Long-term sustainable design with zero structural failure risks, built to withstand demanding industrial maintenance loads.
Authenticity Guaranteed: Regulated factory assembly ensures no mechanical debris inside sensitive, high-capacity refrigeration circuits.
Applications:
Large-scale commercial food processing cold stores.
Multi-compressor industrial refrigeration distribution hubs.
High-demand retail display and backup storage infrastructure.
Technical Specifications
| Attribute | Detail |
| Brand | Industrial Std |
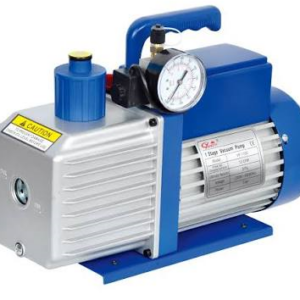
| Trade Name | Protected Heavy-Duty Vacuum Pump (6 CFM) |
| Model | PHVP-6CFM |
| Capacity | 6 CFM Heavy-Duty Protected |
| Application | Heavy-Duty Protected Evacuation |
| Country of Origin | Global Standard |
Logistics & Shipping
Net Weight: 12.5 kg
Gross Weight: Approx. 14.0 kg
Packaging Dimension: 42.0 cm x 24.0 cm x 30.0 cm
Shipping Method: Industrial Freight. Warning: Utilize protective roll cage handles when lifting to prevent strain and impact.
Market Insight: A trusted, budget-friendly bulk solution widely utilized by large-scale commercial cold room operators across Nigeria to manage massive inventory volumes while effectively controlling operational overhead.)